Why Are Gate Valve Seats Important?
Gate Valve Seats are easy to overlook because they sit inside the body, out of sight during routine operation. Yet these surfaces help control leakage when the valve closes. In water lines, power plants, and process facilities, even a small defect can mean persistent seepage, pressure loss, or an unexpected shutdown. The seat is not the whole story; disc alignment, operating conditions, and maintenance matter too. But the contact between seat and gate deserves close attention.
The scale of corrosion-related damage gives this small component a wider context. NACE International’s 2016 IMPACT study estimated global corrosion costs at about US$2.5 trillion annually, or 3.4% of global GDP. That figure covers many industries and components, not gate valve seats specifically. Still, it shows why material choice and condition monitoring matter. API 600 covers design requirements for steel gate valves, while API 598 addresses inspection and testing, including closure performance. These standards provide a stronger basis than appearance alone. A clean-looking seat may still leak. In practice, engineers consider service fluid, temperature, pressure, cycling frequency, and the consequences of leakage before selecting or replacing seat materials. This article explains why Gate Valve Seats matter, what can cause their performance to decline, and which checks help identify trouble early. Some failures are not obvious. That is worth remembering. A seat can be a small part, but overlooking it can turn a minor leak into costly maintenance.
What Is a Gate Valve Seat, and Where Does It Seal?
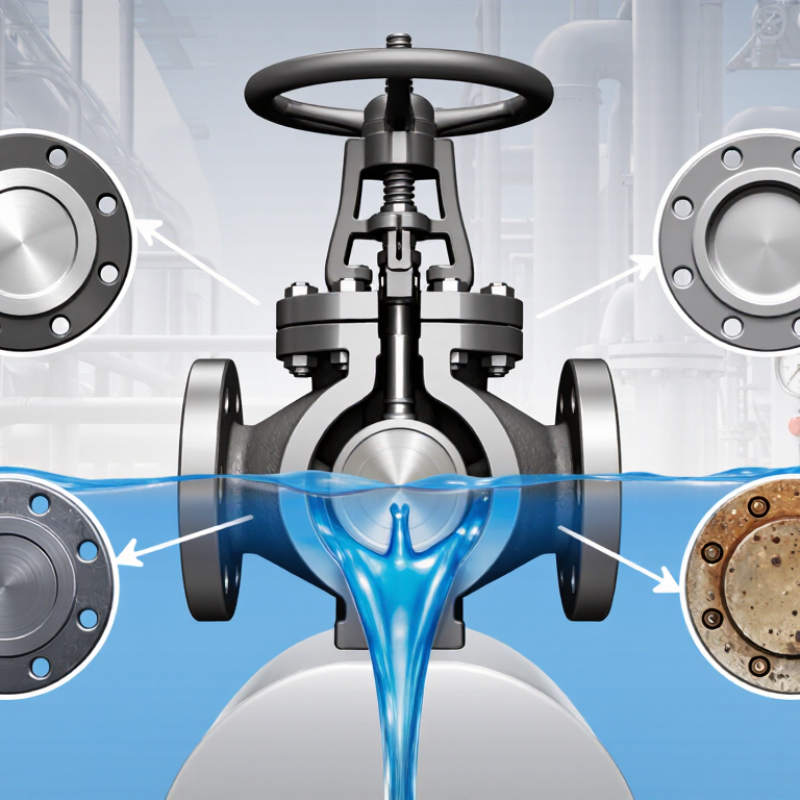
A gate valve seat is the stationary surface inside the valve body that meets the gate when the valve closes. Think of it as a narrow sealing track around the flow opening. The gate moves down between the body’s two sides, and its faces press against the seats to restrict flow. The seal forms here. Not at the handwheel, and not along the stem.
Many gate valves have a seat on each side of the gate, so they can seal against pressure from either direction. In a wedge gate valve, the wedge pushes firmly against angled seats as it descends. Parallel-seat designs use flat sealing surfaces instead. Some seats are metal, while others include a resilient insert; each design suits different service conditions.
Details matter. A scratch across the seat, trapped grit, or slight misalignment can leave a leak path, even when the gate appears fully closed. During inspection, technicians often look for uneven contact marks and deposits around the seating area.
A clean surface helps, but it does not guarantee a tight seal. Pressure, temperature, wear, and the condition of the gate all play a part. Real valves are rarely as tidy inside as a drawing suggests.
How Seat-to-Wedge Contact Stops Flow in a Gate Valve
Why Are Gate Valve Seats Important?
How Seat-to-Wedge Contact Stops Flow in a Gate Valve
Inside a gate valve, the wedge moves down between two seating surfaces as the handwheel or actuator turns the stem. When the wedge meets the seats, their contact creates a barrier across the flow path. The fit must be close and even. A small gap can let liquid or gas pass, even when the valve appears fully closed.
The sealing action depends on the valve’s design. Some metal-seated valves use carefully matched surfaces and closing force to limit leakage. Other designs use resilient materials that compress against the wedge. In either case, pressure, temperature, and the fluid itself affect performance. A technician may look for scoring, corrosion, or trapped grit on the seating faces. A hard particle can hold the wedge slightly open. Tiny details matter.
The idea sounds simple, but seat-to-wedge contact is not a guarantee of perfect shutoff. Wear can change the fit over time, and forcing a stuck valve closed may damage its parts. That point is easy to overlook. Inspection and testing should follow the valve’s service conditions and maintenance guidance. If leakage persists, the seat and wedge may need closer examination rather than extra turning force.
Why Are Gate Valve Seats Important? - How Seat-to-Wedge Contact Stops Flow in a Gate Valve | Dimension | What It Means | How It Affects Shutoff | Practical Inspection Point |
| Seat-to-wedge contact | The sealing interface formed when the closed gate’s wedge bears against the valve seats. | Continuous contact around the sealing surfaces restricts fluid from passing through the closed valve. | Check for an even contact pattern and visible damage on both mating surfaces. |
| Wedge alignment | The wedge must approach the seats in the correct position as the stem closes the gate. | Misalignment can create uneven loading, leaving a leakage path on one side. | Look for asymmetric wear, binding, or damage that may indicate poor alignment. |
| Surface condition | Seat and wedge faces need suitable, undamaged sealing surfaces. | Scratches, corrosion, embedded debris, or erosion can interrupt contact and permit leakage. | Inspect for scoring, pitting, deposits, and foreign material; clean or repair as appropriate. |
| Closing force | The stem and operating mechanism move the wedge into its closed position. | Adequate, correctly applied force helps establish contact; excessive force can damage sealing surfaces or components. | Follow the valve’s operating instructions; do not use added force to compensate for a sticking or leaking valve. |
| Pressure and service conditions | Fluid pressure, temperature, and service conditions influence valve loading and material performance. | Conditions outside the valve’s specified limits can affect sealing reliability and accelerate wear. | Confirm that the valve is rated for the application and inspect it according to the maintenance plan. |
| Debris in the flow path | Solids or residue can collect between the wedge and seats during operation. | Trapped material may prevent full closure or scratch the sealing surfaces. | Assess fluid cleanliness and inspect for deposits when leakage or incomplete closure occurs. |
| Leakage check | A suitable test evaluates whether the closed valve limits leakage under specified conditions. | Observed leakage can indicate damaged surfaces, incomplete closure, debris, or another valve issue. | Use the applicable test procedure and acceptance criteria for the valve and service. |
Which Seat Materials Suit Different Pressure and Service Conditions?
Why Are Gate Valve Seats Important?
The seat forms the sealing surface where a gate closes against the valve body. Its material affects shutoff, operating torque, and resistance to wear. Choosing one by pressure rating alone can lead to leakage or early damage. Temperature, fluid chemistry, solids, and cycling frequency matter too.
For clean water at moderate temperatures, resilient seats such as EPDM can provide tight shutoff. NBR may suit some oil services, while PTFE offers broad chemical resistance but has temperature and load limits. These are starting points, not guarantees. For hot fluids, high pressure, or abrasive particles, metal seats may handle heat and wear better, though they can allow more leakage than soft seats. Compatibility depends on the exact fluid and operating conditions.
Tips: Check the valve’s pressure-temperature limits and the seat material’s chemical compatibility. Ask whether the service contains grit or requires frequent cycling. A material that works in a test can still fail in the field; I would not treat a generic chart as the final answer. Verify selections with the valve supplier’s technical data.
How Seat Wear Can Increase Leakage and Operating Torque
Gate valve seats form the sealing surfaces that meet the gate when the valve closes. When these surfaces are smooth and aligned, they help limit leakage through the closed valve. But wear changes that contact. Abrasive particles, corrosion, repeated cycling, or unsuitable operating conditions can score or pit the seat. Even a narrow groove may leave a path for fluid to pass.
The signs can be subtle. A valve may leak internally despite appearing fully closed, or require more force to operate. Damaged or uneven seats can make the gate bind as it moves, increasing friction and operating torque. Deposits on the sealing area may add resistance too. More force is not always the answer. Forcing a stiff valve can worsen damage to the gate, stem, or actuator, and it may hide the original problem for a while.
Inspection should consider both leakage and the valve’s operating history. Note changes in closing effort, cycle frequency, fluid cleanliness, and pressure conditions. During maintenance, technicians can check for scratches, uneven contact, corrosion, and trapped debris, following the valve manufacturer’s procedures. Seat wear is not always visible from outside. A pressure or leakage test may help confirm whether the valve is sealing as intended. It is worth questioning assumptions: rising torque can also come from packing friction or stem issues, not just the seats.
Why Are Gate Valve Seats Important?
How seat wear can increase leakage and operating torque
Seat wear can reduce sealing contact and allow more fluid to pass through the closed valve. Deposits, galling, or damaged contact surfaces can also increase friction and operating torque. The plotted values are illustrative normalized indices, not test data; actual performance depends on valve design, service conditions, and damage.
How API 598 Tests Seat Tightness at 1.1× Rated Pressure
Why Are Gate Valve Seats Important?
A gate valve seat forms the sealing surface where the gate meets the valve body. Its condition affects shutoff, leakage, and service life. A small scratch, trapped scale, or uneven contact can leave a visible leak path. Seat tightness matters most when the valve is expected to isolate equipment safely.
API 598 includes a high-pressure closure test, commonly conducted at 1.1 times the valve’s rated pressure. The valve is closed, test pressure is applied, and inspectors check for leakage across the seat. For a gate valve, testing may examine each direction, depending on the applicable procedure and valve design. The test medium, duration, and allowable leakage depend on the standard’s requirements and valve type. Details matter. A pressure gauge should be suitable and calibrated, while the test setup must avoid masking leakage. Inspectors may look for droplets at the outlet or monitor pressure changes. A passing test is useful evidence, but it cannot promise perfect performance in every installation. Real pipelines bring vibration, debris, and repeated operation. Honestly, a clean test result can still feel reassuring without telling the whole story. Regular inspection helps connect test data with how the valve actually behaves.